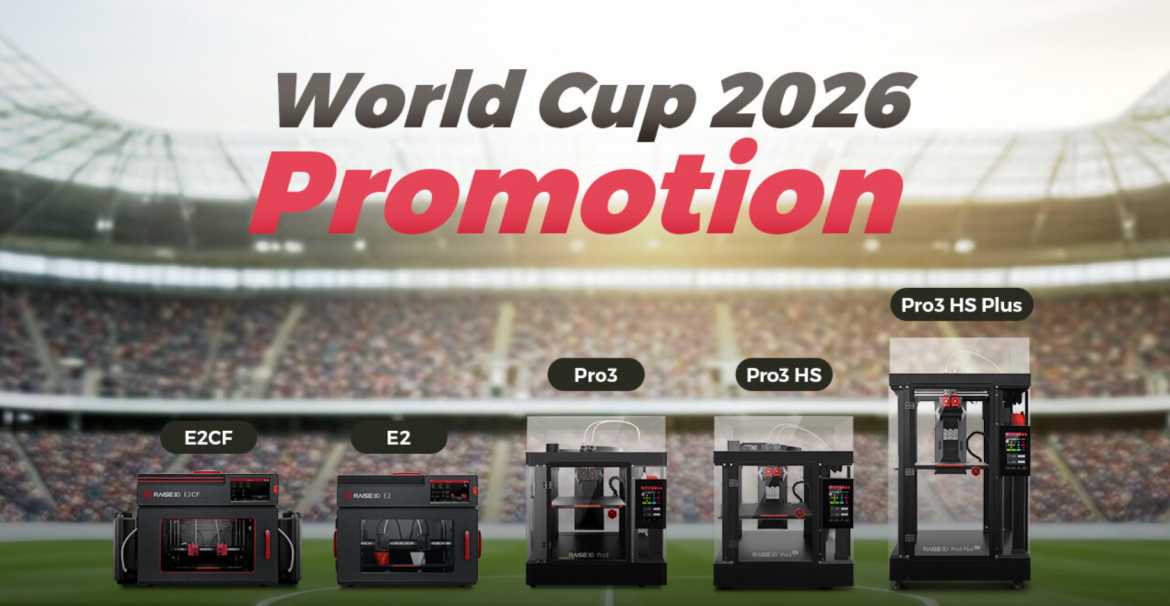
Push hard, but choose smart — that’s the mantra when prototypes must survive real-world stress. Emerging macro trends in aerospace, automotive, and medical prototyping are driving teams to weigh certified selective laser sintering against advanced FDM platforms. The shift is visible on production floors where GE Aviation’s adoption of additive parts for engines moved prototypes into serial-use conversations — and where enclosed work environments like an enclosed fdm 3d printer can actually close the gap on repeatability. Meet the machine punching above its weight: raise3d pro 3 sits in that sweet spot of accessibility and control. I’ll break this down fast, with direct comparisons you can act on today.
Why certified SLS often wins for high-spec parts
Certified SLS delivers consistent, near-isotropic strength and fine feature fidelity — critical for load-bearing aerospace brackets and implant prototypes. The process skips layer-by-layer bonding weaknesses, so parts show fewer directional weaknesses and reduced material porosity. For medical devices where biocompatible powders are a must, the validated material lists and process controls give regulatory engineers confidence. Expect tighter tolerances and complex internal lattices with SLS. The trade: longer lead times and higher per-part cost. Stay on form: choose SLS when the part’s mechanical profile and regulatory traceability are non-negotiable.
Where high-grade FDM like the Raise3D Pro 3 fights back
FDM has levelled up. Modern systems offer enclosed build chambers, active thermal management, and dual extrusion for soluble support strategies. That reduces warping and opens multi-material prototypes that mimic assemblies. Layer height control and robust firmware deliver repeatable prints at lower cost. For many automotive fixtures, jigs, and preliminary medical tooling, a tuned FDM workflow accelerates iteration cycles — and the capital outlay stays manageable. Use FDM when speed, cost per iteration, and accessibility matter most.
Practical trade-offs on the shop floor
Compare directly. SLS: high fidelity, powder handling, post-process sintering. FDM: fast setup, straightforward post-processing, lower material expense. Focus on three axes: mechanical requirements, surface finish expectations, and regulatory evidence. — Don’t ignore post-processing time; it can wipe out perceived cycle gains. For the teams I coach, the easiest wins come from matching the process to the test regime: tensile tests demand SLS in many cases; fit-checks are perfect for FDM.
Common mistakes and quick wins
Teams often over-commit to a single technology. That costs time. Common mistakes: underspecifying support strategies, ignoring thermal management, and skipping proper orientation analysis. Quick wins include optimizing layer height for function (not aesthetics), using soluble supports on complex geometries, and validating build orientation with a short-run test. In an operational production teardown, focus explicitly on {main_keyword} and {variation_keyword} to isolate where defects originate and where process control must tighten.
Three golden rules — evaluation metrics to choose the right tool
1) Functional fidelity score: quantify how closely a printed part meets mechanical targets (tensile, fatigue, dimensional deviation). Use that score to gate SLS vs. FDM. 2) Throughput cost per validated piece: include machine time, post-processing, and inspection labor — pick the method that meets sprint cadence without hidden downstream costs. 3) Regulatory traceability index: measure how easily material certifications, lot tracking, and process logs can be produced for audits. Higher index favors certified SLS; mid-range often suits controlled FDM environments like the raise3d pro 3.
Final take: match tools to purpose, iterate like you train — fast sets for fit, heavy sets for final strength. Raise3D offers that controlled, gym-like environment for printing: repeatable, accountable, ready to push prototypes from idea to test — and that’s the kind of equipment that keeps teams sharp. –